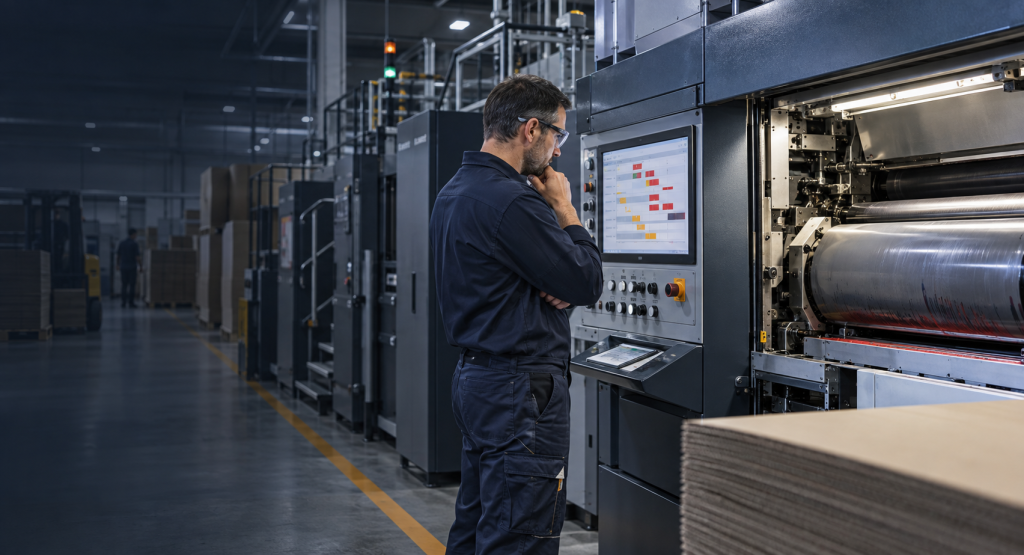
A color change that takes longer than planned. Start-up sheets that end up in the trash. Variations in quality that an operator has to correct on the fly. For most plant managers, these aren’t incidents. It happens every shift, and it’s also noted in the report every shift—as a malfunction, change, or adjustment. What isn’t noted is the cause.
A production report is designed to record what happened, not to explain why. The difference between the two is what this article is about.
What you see, and what's really happening
A color change or a startup sheet is the visible result. The cause runs deeper. An anilox roller that runs below its nominal cell volume for too long transfers less ink than the design requires. A cleaning routine that isn’t quite thorough enough leaves residue in the cells. Both of these factors cause the press to take longer to start up, and the print quality to fluctuate longer before stabilizing.
That takes more than the few minutes mentioned in the report. Longer setup times and extra waste drive down your OEE, shift after shift.
Why the cleaning bill never shows up in the mail
In most factories, cleaning isn't a separate process. It's a task performed between two orders by whoever is on duty at the time, and then the press starts running again. It's rare to measure what the roll did before and what it does afterward.
This creates a blind spot. The effect of cleaning is indeed reflected in the figures, but it’s listed under a different name: malfunction, change, or adjustment. Anyone looking for the cause in those three columns is looking in the wrong place.
What the total comes to when you check the math
Our benchmark study of corrugated cardboard plants shows that about 10% of planned production time is lost to unplanned downtime. For a plant with one or two lines, that amounts to approximately 600 hours per year, or 75 eight-hour shifts.
If you set your production value at 2,500 euros per hour, that amounts to 1.5 million euros in production value per year. Enter your own hourly rate, and you’ll have the figure for your factory.
No one has yet calculated what portion of that is related to cleaning. That is precisely why it is worth calculating that figure.
The Cleaning Performance Cycle
The Cleaning Performance Cycle is how we eliminate that blind spot. It is based on the Total Productive Maintenance methodology and brings together three elements that are typically addressed separately in practice: the product, the process, and behavior on the shop floor.
The goal isn't to have a clean line at a single point in time. The goal is a cleaning routine that isn't dependent on who's working that day, with results that you can see in the cell volume and in your OEE.
Exactly where waste is hidden varies from factory to factory. In the waste matrix, we list those areas by machine, material, method, and person. That is the topic of the next article in this series.
Where do you start?
The cause only becomes apparent when you examine the cleaning routine and the condition of the anilox itself: what is being cleaned, how often, by whom, and how does the cell volume change before and after?
Do you want to know where your waste is coming from?
Request a free consultation, and together we'll figure out where your profit lies.
You can find more information about the Clean Performance Cycle and the waste matrix here.